
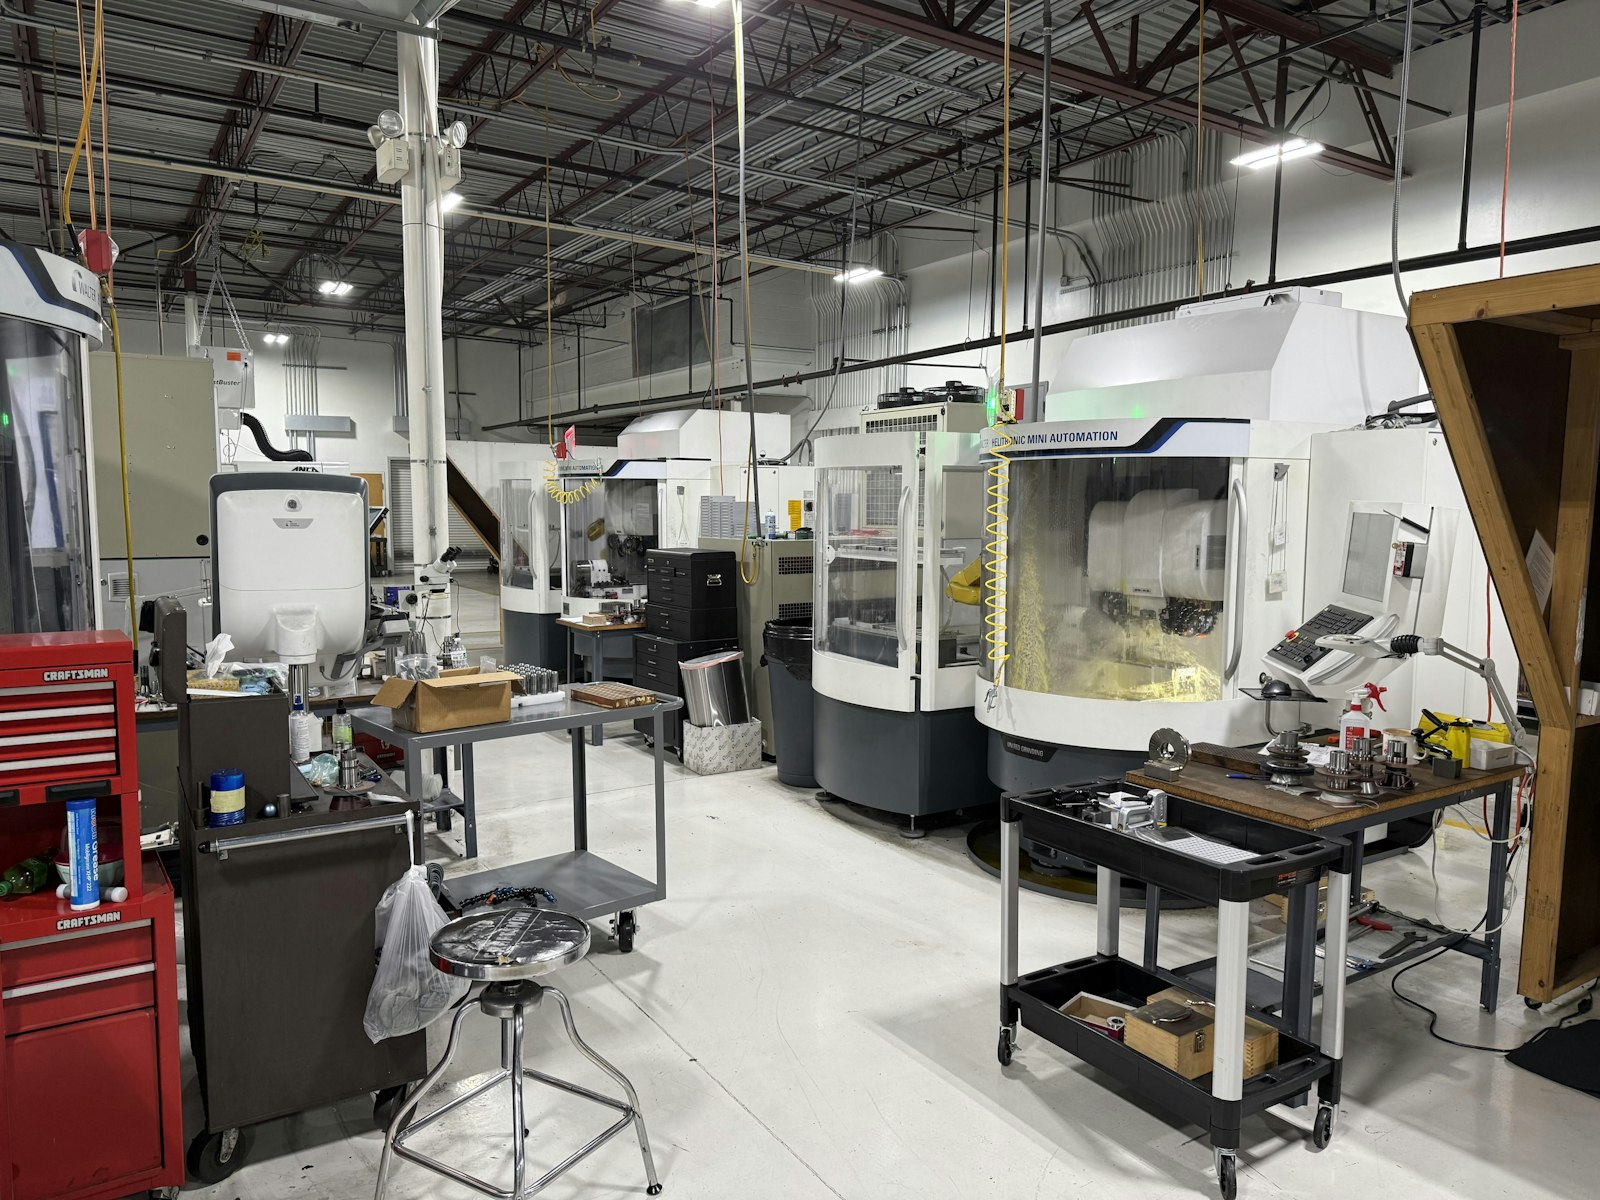
Medical Products That Use TIG Welded Parts
Medical device makers buy welded stainless and titanium parts for a wide range of products. TIG welding suits this work because it gives clean, small, controlled welds on thin material.
Surgical and Procedure Equipment
Instrument trays, sterilizer racks, carts, and stands that see steam, chemicals, and constant handling.
Diagnostic and Lab Equipment
Analyzer frames, fluid manifolds, sample handling parts, and enclosures for lab and imaging systems.
Hospital and Patient Equipment
Bed and chair frames, IV poles, mounts, and arms where welds must be strong and easy to wipe down.
Pharmaceutical and Bioprocess Equipment
Sanitary tube, vessels, and skids built to ASME BPE. See sanitary tube welding.
Compliance Frameworks for Medical Device Suppliers
Device makers own the FDA submission, but suppliers feed the records. These are the frameworks device QA teams check. See the certifications and compliance page.
ISO 13485
The quality system standard for medical devices. It requires supplier controls, traceability, and process validation.
FDA 21 CFR Part 820 (QMSR)
FDA's device quality rule, which now lines up with ISO 13485. Welding is a special process, so device makers must validate it or buy from a supplier who does.
Process Validation (IQ, OQ, PQ)
Welds that cannot be fully checked by later inspection must be validated. That means proving the equipment, the settings, and the output.
Material Standards
Implant and instrument parts often call out ASTM F138 (316LVM bar), ASTM F899 (instrument stainless), or ASTM F136 (Ti-6Al-4V ELI). Biocompatibility follows ISO 10993.
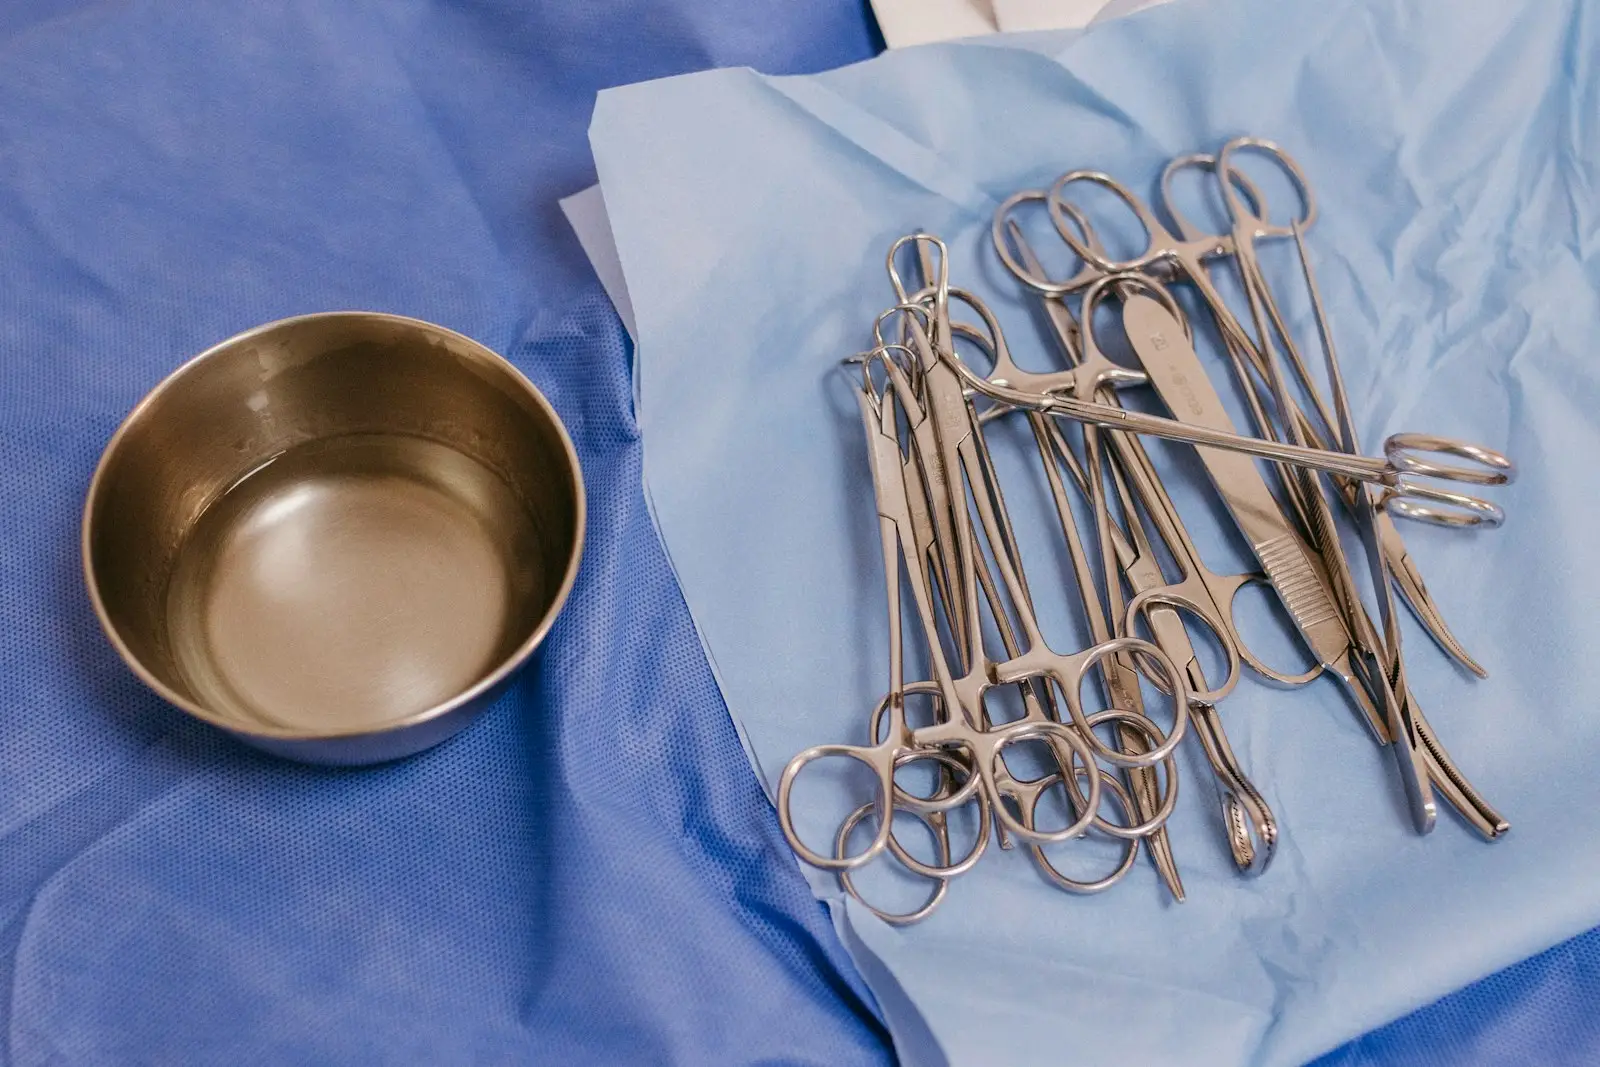 Instrument trays, sterilizer racks, and carts need welds that survive repeated cleaning and sterilization.
Thin-Gauge Medical Welds Without Warpage
Medical parts often run thin wall tube and small features. Too much heat warps them or changes the metal. Our precision stainless TIG service is built for this.
Low-Amp and Pulse TIG
Pulse settings and low amperage keep the heat-affected zone small. Read preventing warpage in thin-gauge stainless.
316L and 316LVM Stainless
Low carbon limits sensitization. 316LVM is vacuum melted for cleaner metal in implant-grade parts. Filler is usually ER316L. Read carbide precipitation in stainless welds.
Titanium Grades 2 and 5
Welded in argon with full trailing and back shielding. Weld color is checked; blue or gray means oxygen pickup and a reject.
Micro TIG and Fixtures
Custom fixtures hold tiny parts still and pull heat away.
Sanitary Tube and Cleanable Equipment
Device makers also need clean process equipment: purified water loops, carts, and wash systems. Our sanitary tube welding and custom stainless fabrication cover these.
- Purge-welded 316L tube with smooth, borescoped interiors
- Stainless carts, frames, and enclosures for clean areas
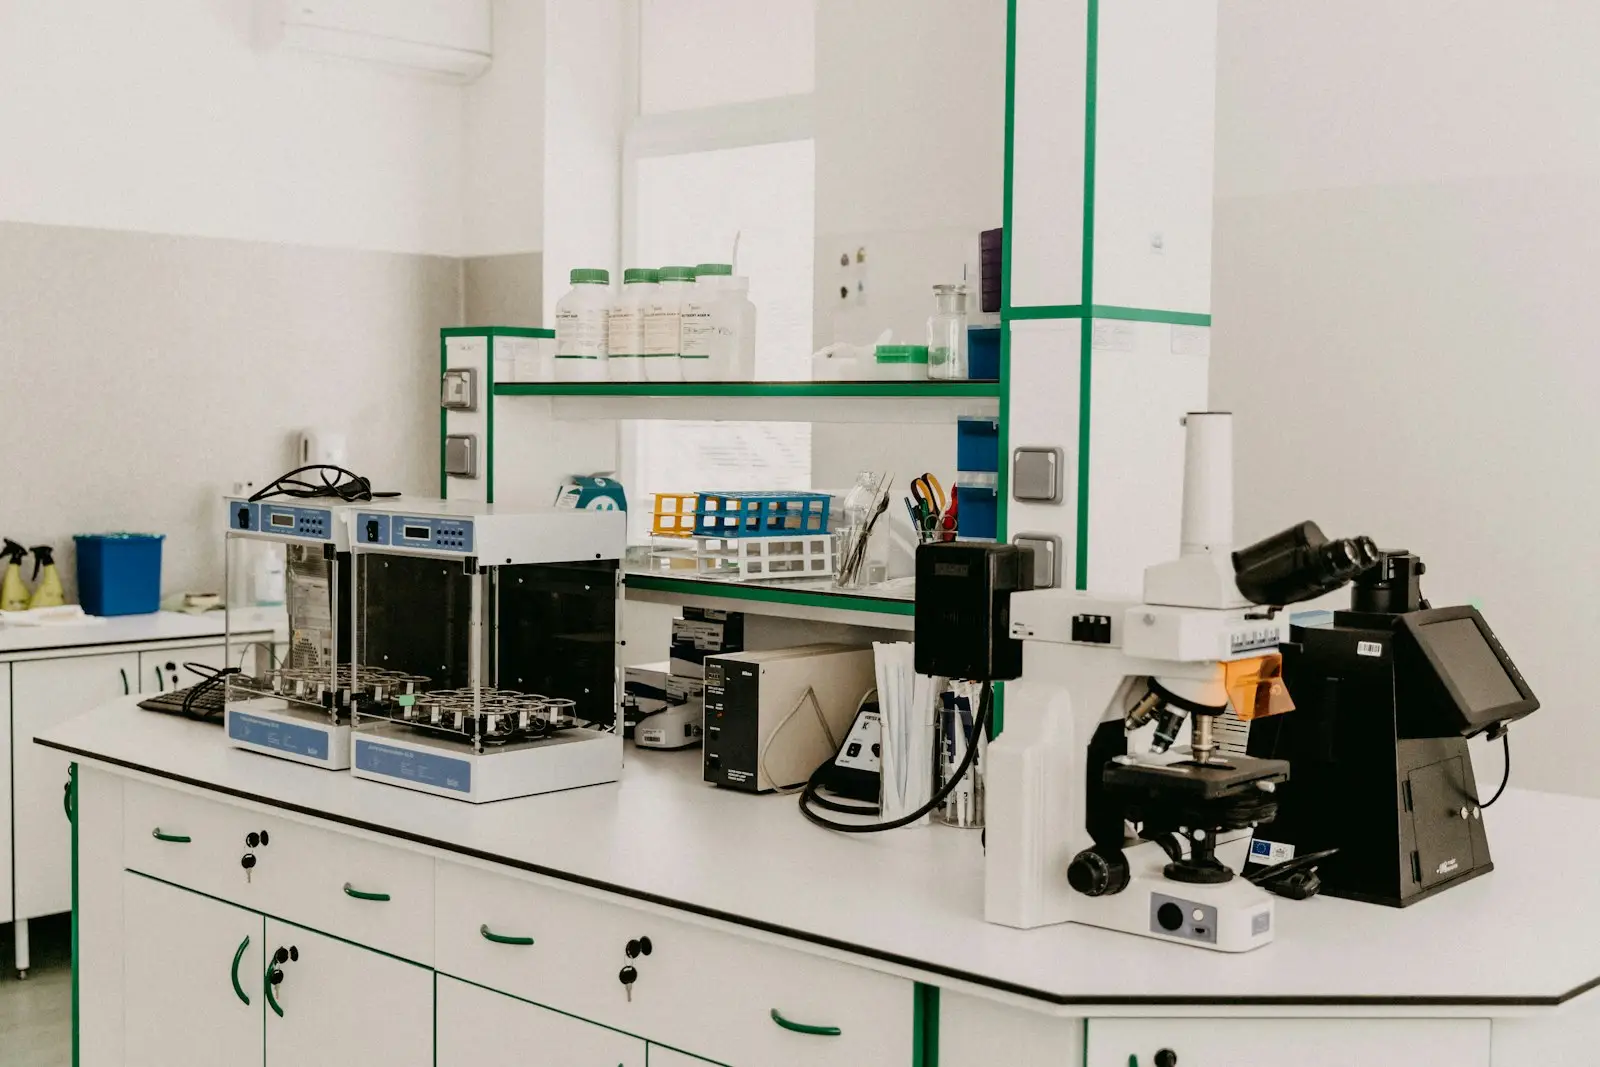 Diagnostic and lab equipment relies on welded frames, manifolds, and enclosures built to tight tolerances.
Cleaning, Passivation, and Biocompatibility
A medical weld is not finished when the arc stops. The surface around it has to be cleaned and restored before the part goes into a device.
Heat Tint Removal
Welding leaves colored oxide next to the bead. That zone is lower in chromium and can rust, so it is removed by mechanical cleaning or pickling.
Passivation
A chemical treatment per ASTM A967 or A380 that removes free iron and helps restore the protective chrome oxide layer.
Electropolishing
An electrochemical process per ASTM B912 that smooths the surface and improves corrosion resistance and cleanability.
Biocompatibility
Testing to ISO 10993 is done on the finished device by the device maker. The welding supplier controls the materials, fillers, and cleaning steps that affect it.
How to Specify Medical Device Welds
Clear requirements up front prevent rework and keep your validation on schedule. Include these with your drawing. For thin parts, read preventing warpage in thin-gauge stainless.
- Drawing and revision, with weld size, location, and acceptance criteria
- Material grade and form, such as 316L, 316LVM, or titanium Grade 2 or 5, with cert requirements
- Validation needs, such as IQ, OQ, and PQ protocols or sample sizes
- Cleaning, passivation, or electropolishing spec, and packaging rules
- Inspection and records needed for your device history record
- Change notification rules for material, process, or location changes
Qualifying a Welding Supplier for Medical Devices
ISO 13485 and the FDA quality system rules require device makers to evaluate and control their suppliers. These are the usual steps for a welding source.
Supplier Evaluation
A review of the supplier's quality system, capability, and history, scaled to the risk of the part.
Quality Agreement
A signed document that sets responsibilities for specs, inspections, records, and change notification.
Process Validation Support
Weld procedures, test coupons, and data that support your IQ, OQ, and PQ.
Ongoing Monitoring
Incoming inspection, audits, and corrective action requests keep the supplier in control after approval.
Serving the Minneapolis Medical Corridor and Beyond
Minneapolis-St. Paul has one of the densest clusters of medical device companies in the U.S. We serve device makers there and nationwide from our Dallas headquarters. A Minneapolis location page is planned.
Frequently Asked Questions
Does my welding supplier need ISO 13485?
Not always. ISO 13485 applies to the device maker. You can use an ISO 9001 supplier if your supplier controls and process validation cover the welding. Many device makers still prefer ISO 13485 suppliers to cut audit work.
Why is welding called a special process for medical devices?
You cannot fully check a weld's inside quality without cutting it apart. So the process itself must be validated to prove it makes good welds every time. That is why device makers ask for IQ, OQ, and PQ data.
What stainless grade is used for medical devices?
316L is common for equipment and instruments. 316LVM, a vacuum-melted version per ASTM F138, is used for implants. Some instruments use martensitic grades such as 420, which need different welding rules.
How thin can you TIG weld stainless tube?
Very thin wall needs low-amp pulse TIG, tight fit-up, and fixtures that act as heat sinks.
Can you support our device history records?
Yes. We can supply MTRs, filler lot numbers, welder IDs, WPS numbers, and inspection results per lot.
What is the difference between passivation and electropolishing?
Passivation is a chemical cleaning that removes free iron and helps restore the chrome oxide layer without changing the surface texture. Electropolishing removes a thin layer of metal, so it also smooths the surface. Both improve corrosion resistance.
Why do device makers validate welding instead of inspecting every weld?
Many weld defects are inside the joint and cannot be found without cutting the part apart. When results cannot be fully checked by inspection, FDA rules and ISO 13485 require the process to be validated and then kept within validated limits.
What is a quality agreement with a welding supplier?
A quality agreement is a written contract between the device maker and the supplier. It spells out specs, inspections, records, and what the supplier must report before changing a material or process.
