
Where TIG Welding Is Used in Oil, Gas, and Petrochemical Plants
Most heavy pipe is filled and capped with faster processes, but TIG welding handles the root pass, thin wall, small bore, and alloy work. These are the most common uses. See pipe and pressure vessel welding.
Process Piping Spools
Shop-built spools for refineries and chemical plants, with TIG root passes for full, clean penetration.
Instrument and Chemical Injection Tubing
Small-bore stainless tube and fittings, where TIG gives the control needed on thin wall.
Skids and Modules
Metering, injection, and filtration skids with piping, frames, and supports welded and tested as one unit.
Pressure Vessel and Exchanger Components
Nozzles, small vessels, and heat exchanger parts built to ASME Section VIII.
Compliance Frameworks for Plant Piping and Vessels
Owner specs in refining and chemicals build on public codes. These are the ones your inspector will check. See the certifications and compliance page.
ASME Section IX
Qualifies welding procedures (WPS, PQR) and welders (WPQ). Read ASME Section IX for pressure vessel TIG welds.
ASME B31.3 and Section VIII
B31.3 governs process piping. Section VIII Division 1 governs pressure vessels.
NBIC and API Inspection Codes
Repairs to stamped vessels follow the NBIC and need an R stamp. Owners inspect in-service piping and vessels to API 570 and API 510.
NACE MR0175 / ISO 15156
Sets material and hardness limits for sour service with hydrogen sulfide. Welds may need hardness testing to prove they meet it.
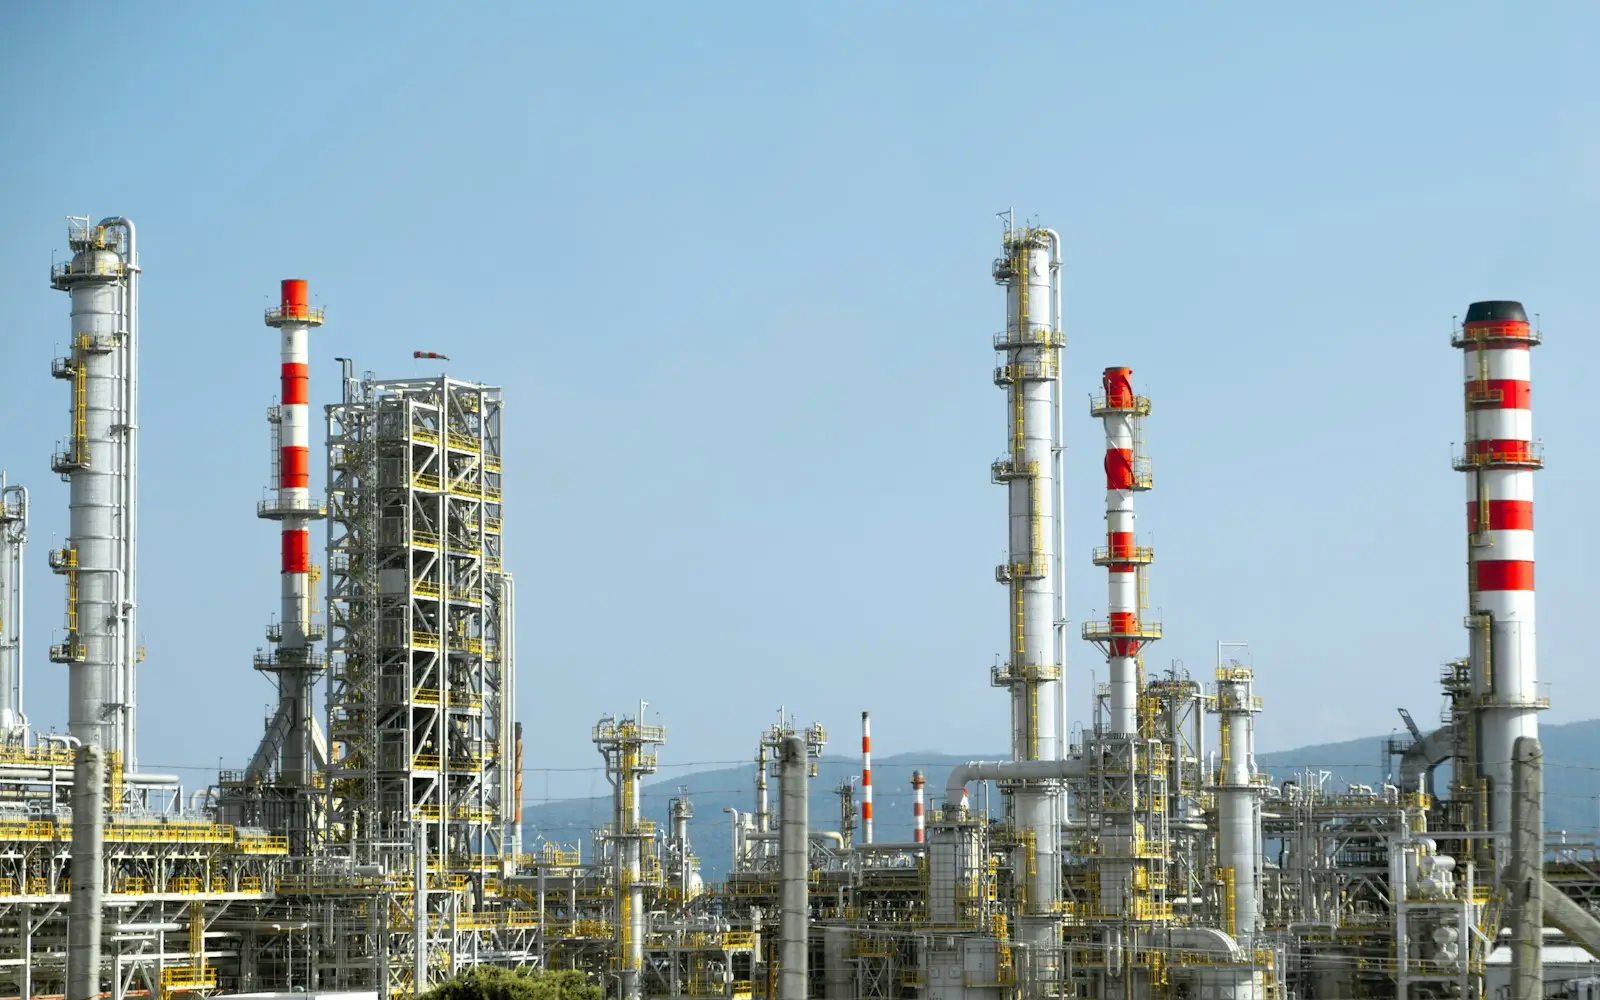 Refinery and chemical plant piping is designed, built, and examined to ASME B31.3.
Pipe and Pressure Welding by Material
Our pipe and pressure vessel welding service covers the main plant alloys.
Carbon Steel Piping
TIG root with ER70S-2 or ER70S-6, then TIG or stick fill and cap per the WPS. The most common plant material.
304L and 316L Stainless
Used for corrosive and low-temperature service. Welded with ER308L or ER316L and a full argon back-purge. Compare fillers in ER308L vs. ER316L.
Chrome-Moly for Heat
P11, P22, and P91 piping for high-temperature service needs preheat, interpass control, and PWHT.
Dissimilar Metal Welds
Stainless to carbon steel tie-ins usually use ER309L. Read welding 304 stainless to carbon steel.
NDE and Testing on Code Welds
The fluid service category in B31.3 sets how much of each exam is needed. Owner specs often add more.
- Visual examination of 100% of welds
- Radiography (RT) or phased-array ultrasonic (PAUT) per ASME Section V
- Liquid penetrant (PT) and magnetic particle (MT)
- Hardness testing for sour service
- PMI on alloy piping to catch mixed-up material
- Hydrostatic or pneumatic leak testing
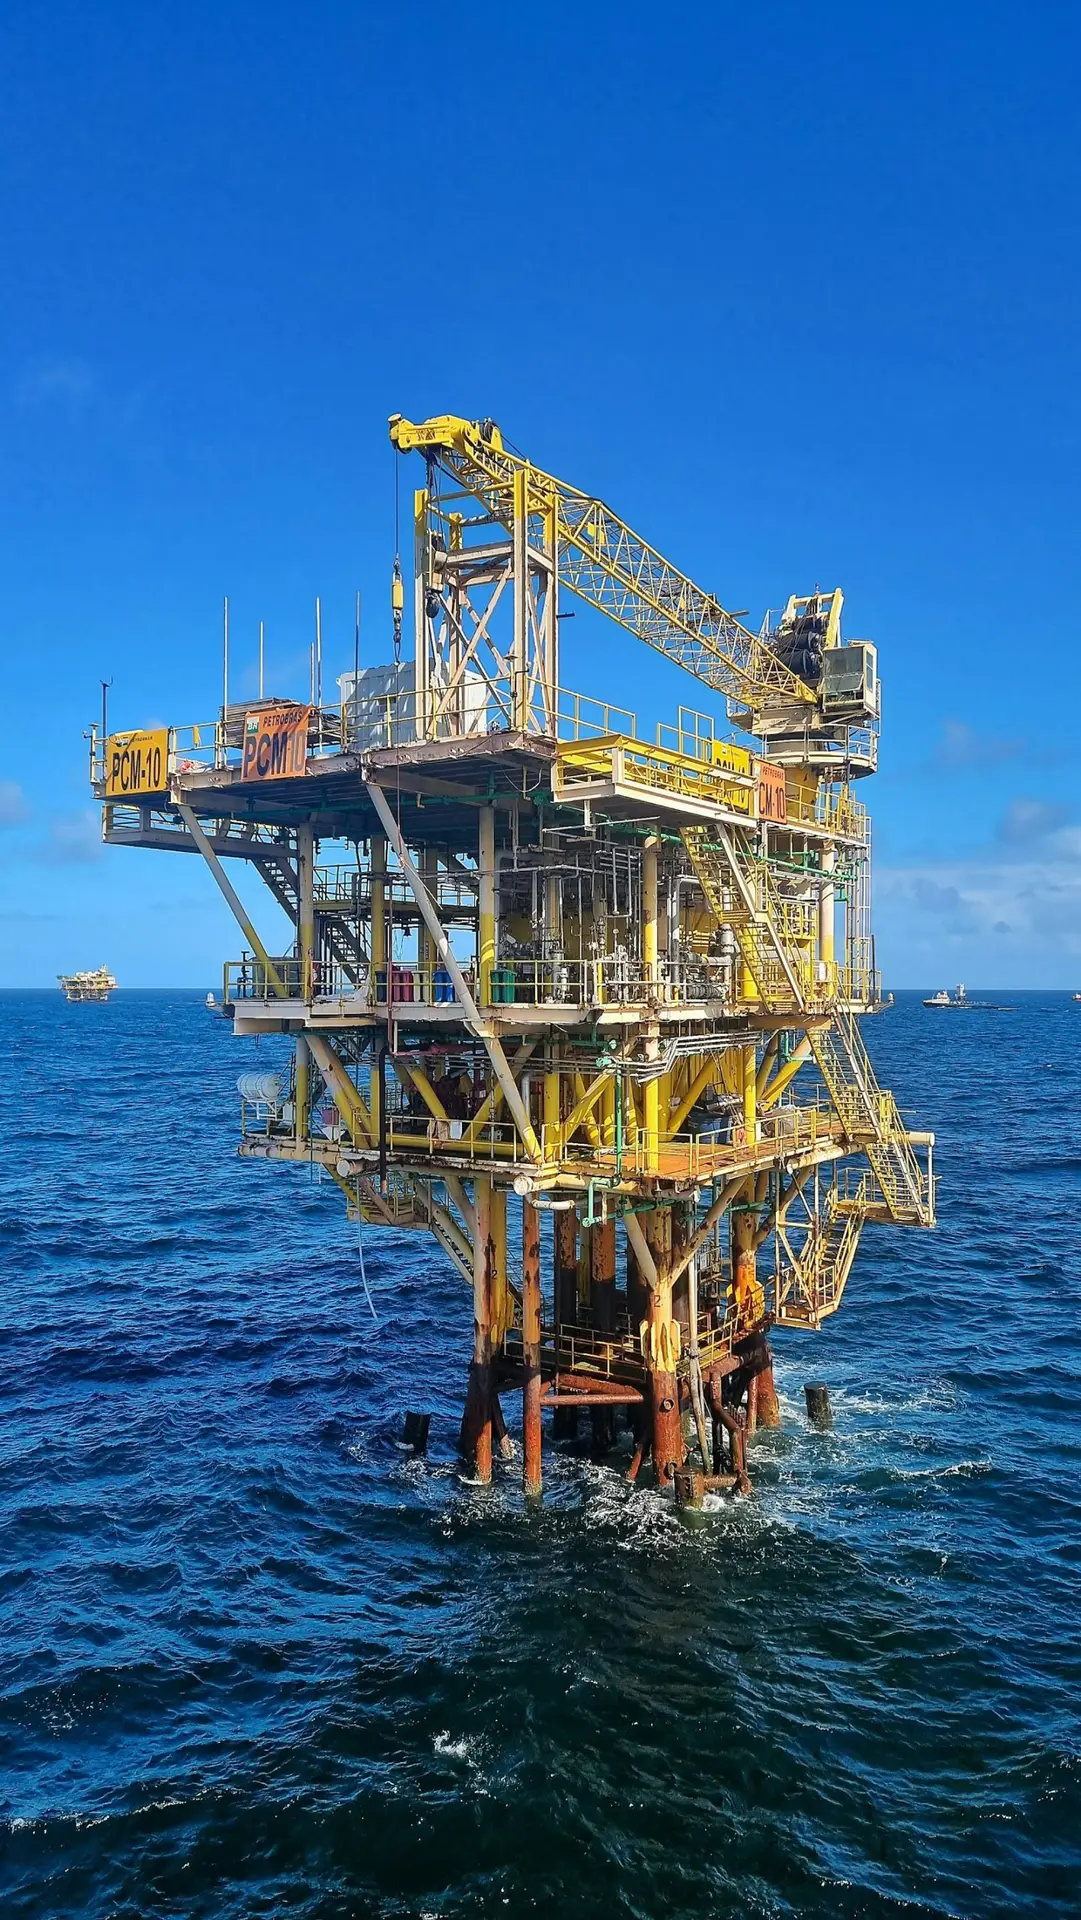 Offshore and Gulf Coast facilities add salt air, chlorides, and sour service to the material choice.
Corrosion and Cracking Risks in Plant Service
Material choice and weld quality decide how long plant piping lasts. These are the damage types engineers design around most often.
Chloride Stress Corrosion Cracking
304L and 316L can crack under stress in warm chloride service. Duplex stainless resists it far better, which is why it is common offshore and in cooling water.
Sulfide Stress Cracking
Hard welds can crack in sour service with hydrogen sulfide. NACE MR0175/ISO 15156 limits hardness, for example 22 HRC for carbon steel.
Sensitization
Too much heat can tie up chromium at grain boundaries and cause intergranular attack. Read carbide precipitation and sensitization.
Galvanic Corrosion at Dissimilar Joints
Where stainless meets carbon steel, the carbon steel side can corrode faster. Read TIG welding 304 stainless to carbon steel.
What Goes in a Code Weld Turnover Package
The turnover package proves that every weld was made and examined to code. Owners and inspectors review it before the system goes into service.
- Weld procedure specifications and their procedure qualification records
- Welder performance qualifications and continuity logs
- Weld map with weld numbers, welder IDs, and procedures used
- Material test reports traced by heat number
- NDE reports, such as radiography, ultrasonic, penetrant, or magnetic particle
- PMI, hardness, and post-weld heat treatment records where required
- Pressure test record signed by the inspector
Choosing a Welding Contractor for Plant Work
Owners and EPC firms look past price when they pick a welding source for code work. These are the points that matter most. Read ASME Section IX for pressure vessel TIG welds for background.
Procedure Coverage
Qualified procedures that cover the P-numbers, thicknesses, and positions in the job, so no new qualification is needed.
Welder Continuity
Welders with current qualifications and continuity records for each process.
Inspection and Test Plan
A written plan with hold points for fit-up, NDE, heat treatment, and pressure testing.
Owner and Site Approval
Approval on the owner's vendor list, a review of their specs, and any site safety prequalification.
Serving Houston and the Gulf Coast
The Houston Ship Channel, Pasadena, Baytown, and Texas City form one of the largest refining and petrochemical hubs in the world. Baton Rouge and the Mississippi River corridor in Louisiana add another major cluster.
We serve plants and fabricators in Houston and along the Gulf Coast from our Dallas headquarters. A Baton Rouge location page is planned.
Frequently Asked Questions
What is the difference between ASME Section IX and B31.3?
B31.3 is the construction code for process piping: design, fabrication, and exams. Section IX is how you qualify the welding procedures and welders that B31.3 requires. You need both on a plant piping job.
Do you need an ASME stamp to weld plant piping?
No. B31.3 piping does not carry a code stamp, but it still needs qualified procedures and welders. A U stamp is needed to build Section VIII vessels, and an R stamp for NBIC repairs.
Why do sour service welds need hardness testing?
Hard welds can crack when exposed to hydrogen sulfide. This is called sulfide stress cracking. NACE MR0175/ISO 15156 sets hardness limits, and hardness testing proves the weld meets them.
Why use a TIG root pass on process pipe?
TIG gives a clean, fully fused root with a smooth inside surface. That lowers the risk of RT rejects and gives less surface for corrosion and buildup. Many owner specs require it on stainless and alloy lines.
Can you support turnaround and shutdown schedules?
Prefabricated spools built in our shop can cut time in the plant.
What is PMI testing?
Positive material identification, or PMI, uses a handheld XRF or OES analyzer to confirm the alloy of pipe, fittings, and weld metal. It catches material mix-ups before alloy piping goes into service.
What is a weld map?
A weld map is a drawing or log that numbers every weld and records the welder, the procedure, and the examination results for each one. It ties the turnover package together.
Why is duplex stainless used in chloride service?
Duplex stainless such as 2205 resists chloride stress corrosion cracking and pitting much better than 304L or 316L, and it is about twice as strong. Welding it needs controlled heat input to keep the right balance of ferrite and austenite.
