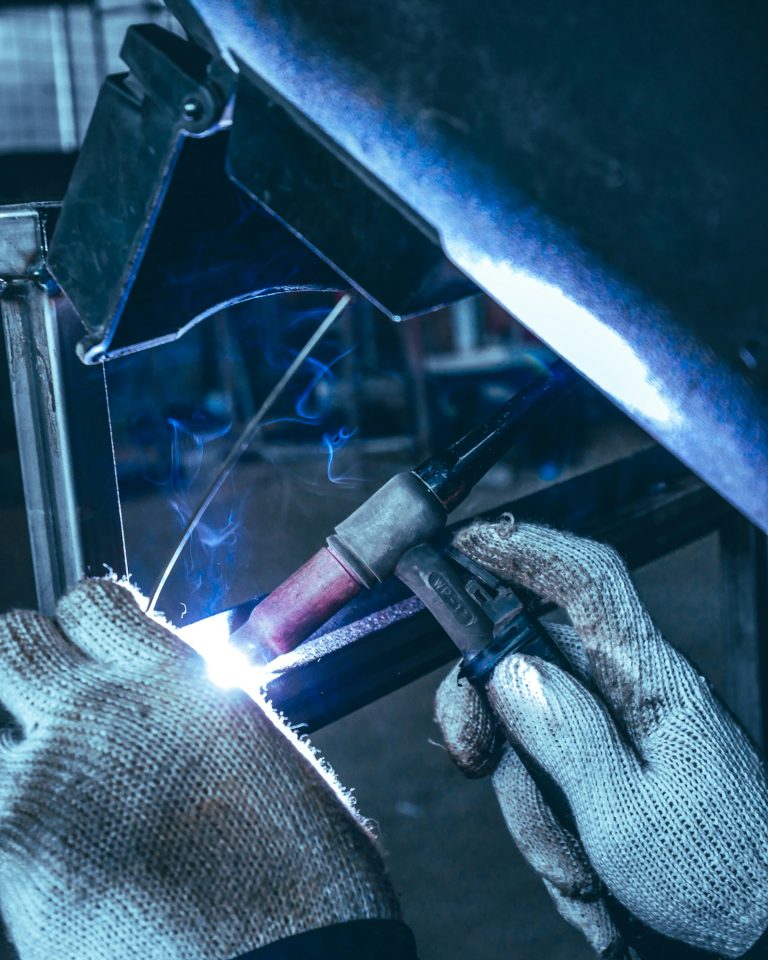
Use ER309L filler rod to TIG weld 304 stainless steel to carbon steel. Its extra chromium and nickel absorb the dilution from the carbon steel side, so the finished weld stays a tough, crack-resistant austenitic stainless instead of turning hard and brittle.
Filler choice is only part of the job. The two metals expand at different rates, move heat at different rates, and corrode each other when wet. This guide covers each problem and gives a step-by-step setup for manual TIG (GTAW).
Why use ER309L instead of ER308L or carbon steel filler?
When you weld two different metals, the weld puddle is a mix of the filler and both base metals. On the carbon steel side, the base metal adds iron and carbon but no chromium or nickel. That pulls the alloy content of the weld down.
- Carbon steel filler (ER70S-2 or ER70S-6) picks up chromium and nickel from the 304. The result can be hard martensite that cracks, and the weld has no stainless corrosion resistance.
- ER308L has just enough alloy to match 304. Once carbon steel dilutes it, the weld metal can drop into the martensite zone and crack.
- ER309L starts with more chromium and nickel. After dilution, it still lands in the austenite zone with a small amount of ferrite. That ferrite helps the weld resist hot cracking as it cools.
| Filler | Chromium (wt %) | Nickel (wt %) | Result on a 304-to-carbon-steel joint |
|---|---|---|---|
| ER70S-6 | Residual only | Residual only | Risk of hard, crack-prone weld; no corrosion resistance |
| ER308L | 19.5 to 22.0 | 9.0 to 11.0 | Too little alloy margin after dilution; cracking risk |
| ER309L | 23.0 to 25.0 | 12.0 to 14.0 | Austenite with some ferrite; the standard choice |
Ranges shown are typical AWS A5.9 classification limits. Both L-grade fillers carry 0.03% maximum carbon. For more on the 300-series fillers, see ER308L vs. ER316L filler rods.
What is dilution, and how do you control it?
Dilution is the share of the finished weld metal that came from melted base metal rather than the filler rod. More dilution from the carbon steel side means less chromium and nickel in the weld.
Engineers estimate the final weld chemistry with a constitution diagram, such as the Schaeffler diagram or the WRC-1992 diagram. You plot the 304, the carbon steel and the filler by their chromium and nickel equivalents. You then draw a line between them and mark the expected dilution. The point where the weld lands shows whether it will be austenite, ferrite, martensite or a mix. A good plan lands in austenite with a few percent ferrite.
To keep dilution low with TIG
- Always add filler. Never fuse the joint without rod (an autogenous weld) on a dissimilar joint.
- Keep heat input low. Heat input in J/in equals volts times amps times 60, divided by travel speed in in/min.
- Keep the arc on the leading edge of the puddle and feed rod steadily. Some welders bias the arc slightly toward the stainless side. Follow the qualified WPS.
- Run stringer beads instead of wide weaves.
- For thick or critical joints, butter the carbon steel bevel first. Lay one or two layers of ER309L on the carbon steel face, then fill the joint.
How do thermal expansion and heat flow affect the joint?
Austenitic stainless grows more when hot and holds heat longer than carbon steel. Typical values are below.
| Property (typical) | 304 stainless | Carbon steel (A36 / 1018) |
|---|---|---|
| Thermal expansion, 70 to 212 °F | About 9.6 µin/in per °F | About 6.5 µin/in per °F |
| Thermal conductivity | About 9.4 BTU/hr·ft·°F | About 29 BTU/hr·ft·°F |
| Melting range | About 2,550 to 2,650 °F | About 2,600 to 2,800 °F |
These are handbook values for annealed material. Check the data sheet for your exact grade. Here is what they mean at the torch
- The stainless side melts first. It holds heat near the arc, while the carbon steel wicks heat away. Watch that both sidewalls fuse.
- The stainless side shrinks more. It expands about 50% more, so it pulls the part toward the stainless as it cools. Tack closely, use a fixture, and balance your weld sequence.
- Thermal cycling strains the joint. Parts that heat and cool in service see stress at the fusion line every cycle. For hot or cycling service, see the section on when ER309L is the wrong choice.
Thin parts warp easily. Our guide on preventing warpage in thin-gauge stainless covers chill blocks, pulse TIG and stitch welding.
How do you prevent galvanic corrosion at the joint?
Passive stainless steel is more noble than carbon steel. When the joint is wet with water, condensate or process fluid, the two metals form a battery. The carbon steel is the anode and corrodes faster than it would alone. A small area of carbon steel next to a large area of stainless corrodes fastest.
- Keep the joint dry where you can, and design out water traps.
- Coat the joint. If you can coat only one side, coat the stainless (the cathode) or coat both. Run the coating across the weld and onto the stainless. Coating only the carbon steel leaves pinholes as tiny anodes that corrode quickly.
- Keep tools separate. Use stainless-only wire brushes and grinding discs on the 304. Carbon steel dust pressed into stainless will rust and stain it.
Step-by-step: TIG setup for 304 to carbon steel
- Clean both sides. Grind mill scale, rust, paint and oil off the carbon steel back at least 1 in from the joint. Wipe both sides with acetone. Use a stainless-only brush on the 304.
- Fit up. Bevel and gap per the drawing or WPS. Keep the root gap even so the puddle wets both sides.
- Set up gas. Use 100% argon shielding. A common starting point is 15 to 20 CFH with a standard cup; a gas lens may need a different rate. On full-penetration joints, back purge the root with argon so the stainless root does not oxidize. See preventing sugaring.
- Choose rod and tungsten. Use ER309L sized to the joint, often 1/16 in or 3/32 in. Use a 2% lanthanated or ceriated tungsten on DCEN.
- Check preheat and interpass. Thin mild steel usually needs no preheat. Thick or higher-carbon steel may need preheat to avoid hydrogen cracking; follow the WPS. Keep interpass temperature within the WPS limit.
- Weld. Run stringer beads, feed rod steadily, and keep the arc short.
- Finish. Remove heat tint from the stainless side by mechanical cleaning or pickling. Inspect the weld, then coat the joint.
When is ER309L the wrong choice?
ER309L covers most room-temperature and moderate-temperature joints. It is not the answer for every case.
- High temperature or heavy thermal cycling. In hot service, carbon migrates from the carbon steel into the weld, and the expansion mismatch strains the fusion line. Engineers often switch to a nickel-based filler such as ERNiCr-3 for these joints.
- Post-weld heat treatment. If the carbon steel needs stress relief, the 304 spends time in the sensitizing range of about 800 to 1,600 °F. L-grade stainless lowers the risk. Another option is to butter the carbon steel bevel (often with a nickel-based filler), heat treat that part, and then weld it to the 304 with no further heat treatment. See our post on carbide precipitation and sensitization.
- 316 or 316L to carbon steel. Use ER309LMo so the weld keeps molybdenum for chloride resistance.
- Code work. On ASME work, a 304-to-carbon-steel joint is a P-No. 8 to P-No. 1 joint and needs its own qualified WPS. See ASME Section IX for pressure vessels.
What is buttering, and when should you use it?
Buttering means depositing one or more layers of filler on the carbon steel joint face before the parts are fitted together. The final joint is then welded between the buttered layer and the stainless side. For a 304-to-carbon steel joint, the butter layer is usually ER309L.
Buttering helps in several situations
- Controlling dilution: the butter layer absorbs carbon steel dilution, so the final weld bead lands on stainless-type metal and keeps the right chemistry.
- Separating heat treatments: when the carbon steel part needs post-weld heat treatment, it can be buttered and heat treated first. The final joint to stainless is then made without heat treating the stainless side.
- Thick sections: on heavy joints, buttering makes the root and fill passes more predictable.
- Repair and overlay: buttering also restores a worn carbon steel face before it is joined or clad.
For high-temperature or thermal cycling service, a nickel-based filler such as ERNiCr-3 may replace ER309L. Its expansion rate sits between the two base metals and it slows carbon migration. That choice belongs to the design engineer.
How do you inspect a dissimilar metal weld?
Dissimilar joints limit which inspection methods work, so the inspection plan has to account for both metals.
- Visual inspection: works the same as on any weld, checking profile, undercut and cracks.
- Liquid penetrant: works across both metals and the weld, so it is the usual surface crack test.
- Magnetic particle: only works on the carbon steel side. Austenitic stainless and most ER309L weld metal are not magnetic enough.
- Radiography: works across the joint, though the density difference between the metals has to be allowed for when reading film.
- Ultrasonic testing: possible but harder, because austenitic weld metal has coarse grains that scatter sound. It needs special procedures and trained technicians.
- Ferrite check: a ferrite gauge reading on the weld confirms that dilution has not pushed the weld metal toward a crack-prone structure.
After inspection, the carbon steel side still needs corrosion protection. It is usually painted or coated up to the weld.
Where TIGTechs uses this joint
Stainless-to-carbon-steel joints show up on brackets, frames, tank supports, nozzles and machine bases. TIGTechs welds them through our custom stainless fabrication and precision stainless TIG welding services.
Need a mixed-metal assembly built right the first time? Request a quote and include the grades, thicknesses and service conditions. We will recommend the filler and joint design before we cut metal.
Frequently asked questions
Use ER309L for 304 or 304L welded to mild or carbon steel. Its higher chromium and nickel keep the weld austenitic after the carbon steel dilutes it. For 316 to carbon steel, use ER309LMo.
It is not recommended. ER308L has only enough alloy to match 304, so dilution from the carbon steel can push the weld into hard, crack-prone martensite. ER309L gives the margin you need.
Back purge with argon when the joint is full penetration and the stainless root side will be exposed to corrosive service. Without a purge, the stainless root oxidizes and loses corrosion resistance. A partial-penetration or fillet weld usually does not need one.
The carbon steel side will rust like any carbon steel, and it can corrode faster near the stainless when the joint is wet. Coat the joint, running the coating across the weld onto the stainless. Keep the stainless free of carbon steel dust.
Consider a nickel-based filler such as ERNiCr-3 for joints in high-temperature service, heavy thermal cycling, or where the assembly will be heat treated after welding. It reduces carbon migration and better matches the expansion of carbon steel.
It is possible, but it needs engineering review. During heat treatment, carbon migrates from the carbon steel into the stainless weld metal, and the stainless side can sensitize. A common way around this is to butter and heat treat the carbon steel part first, then make the final joint without heat treatment.
The stainless side benefits from it, but passivating acids attack carbon steel, so the assembly can’t be dipped as a whole. Shops mask the carbon steel and passivate the stainless side locally with gel or an electrochemical cleaner, then coat the carbon steel.